Start With What Changed
Good VFFS troubleshooting starts before you touch a setting. Write down three things:
- The symptom, exactly as you see it: which bags, how often, from which point in the run.
- The alarm, if there is one: the code and text on the HMI, with a photo of the screen.
- What changed before it started: a new film batch, a new product or fill weight, a changeover, a cleaning, a new operator, a parts replacement or a change in air or power supply.
Most stops trace back to a change in the film, the product, a setting or a worn part. Changing several settings at once to chase the symptom makes the cause harder to find.
Common VFFS Faults and Where to Look
| Symptom | Common causes | First checks |
|---|---|---|
| Bag length varies, print drifts out of register | Photo eye dirty or misaligned, print mark hard to read, pull belts slipping or worn, film too slick on the outside | Clean and re-teach the photo eye, check belt wear and pressure, compare the film batch with the last good one |
| Film wanders sideways on the tube | Roll not centered, uneven tension, film wound unevenly, worn belts | Recenter the roll, check the unwind tension (dancer, brake or powered unwind), try a roll from another batch |
| Wrinkles at the forming shoulder | Film too grippy on the inside, damaged shoulder, wrong forming set for the film width | Inspect the shoulder for burrs and dents, check the forming set matches the film |
| Weak or leaking cross seals | Jaw temperature, pressure or dwell too low for the film, product in the seal area, dirty or damaged jaws | Check jaw temperatures against the setpoints, clean the jaws, check the product drop timing |
| Leaking back seal | Back seal temperature or pressure, film overlap off, back seal bar worn | Check overlap and tracking first, then temperature and pressure |
| Product caught in the cross seal | Dose arriving late, long product drop, sticky or dusty product | Check the timing between the doser and the jaws, and the drop height |
| Film breaks | High drag at the shoulder, splice or defect in the roll, tension too high | Look at where the break starts, check the roll for defects and the tension settings |
| Bags not cut cleanly | Worn or dull knife, knife timing, film too thick or tough for the knife | Inspect and replace the knife, check timing |
| Empty bags or double doses | Doser and bagger signals out of step | Check the handshake between the doser and the bagger before adjusting either |
Registration and bag length problems often start with the film: Packaging Film COF for VFFS explains how a film that is too slick or too grippy shows up on the machine. Leaking seals are covered in Why Frozen Food Bags Leak at the Seal.
Electrical Troubleshooting: Sensors, Heaters and Drives
Electrical faults usually announce themselves with an alarm. Use the alarm code as a starting point. A drive alarm can be caused by a mechanical jam, and a temperature alarm by a loose sensor connection rather than a failed heater.
Common sources:
- Sensors: photo eyes, proximity sensors and door switches that are dirty, loose or knocked out of position.
- Heating: heaters, temperature sensors and their wiring in the sealing jaws, which work hard and move on every cycle.
- Servo drives and motors: alarms from overload, position errors or a jam the drive is reporting.
- Air supply: low or unstable air pressure behind pneumatic cylinders, such as knives, gusset fingers or jaws on pneumatic machines.
- Interlocks: guards and safety circuits that stop the machine when a door is open or a switch has failed.
Isolate and lock out the machine and release the air pressure before opening any guard or electrical cabinet, and leave work inside the cabinet to a qualified electrician. Before changing a part, photograph the alarm history. Intermittent faults are much easier to trace from that record than from memory.
What Causes the Most VFFS Downtime
Breakdowns get the attention, but on many lines they are not where most of the time goes. Look at where the hours are actually lost:
- Changeovers of forming sets, bag lengths and settings.
- Film roll changes, and the bags rejected after each one.
- Cleaning, especially with sticky, oily or dusty products.
- Small stops: short jams and alarms that are cleared in a minute but happen many times a shift.
- Waiting for parts that were not in stock.
Small stops rarely appear in the breakdown log, but they add up. Count them for a week before deciding what to fix. What Determines Actual VFFS Packaging Speed? explains how these stops turn a machine maximum into the output you actually get.
A VFFS Maintenance Routine That Prevents Repeat Faults
No single interval suits every machine; it depends on the duty, the product, the environment and the machine's history. Most routines cover these points:
- Every shift: once the jaws have cooled and the machine is isolated, clean the sealing jaws and the area around them, clean the photo eye, check for product build-up on the forming tube and chutes.
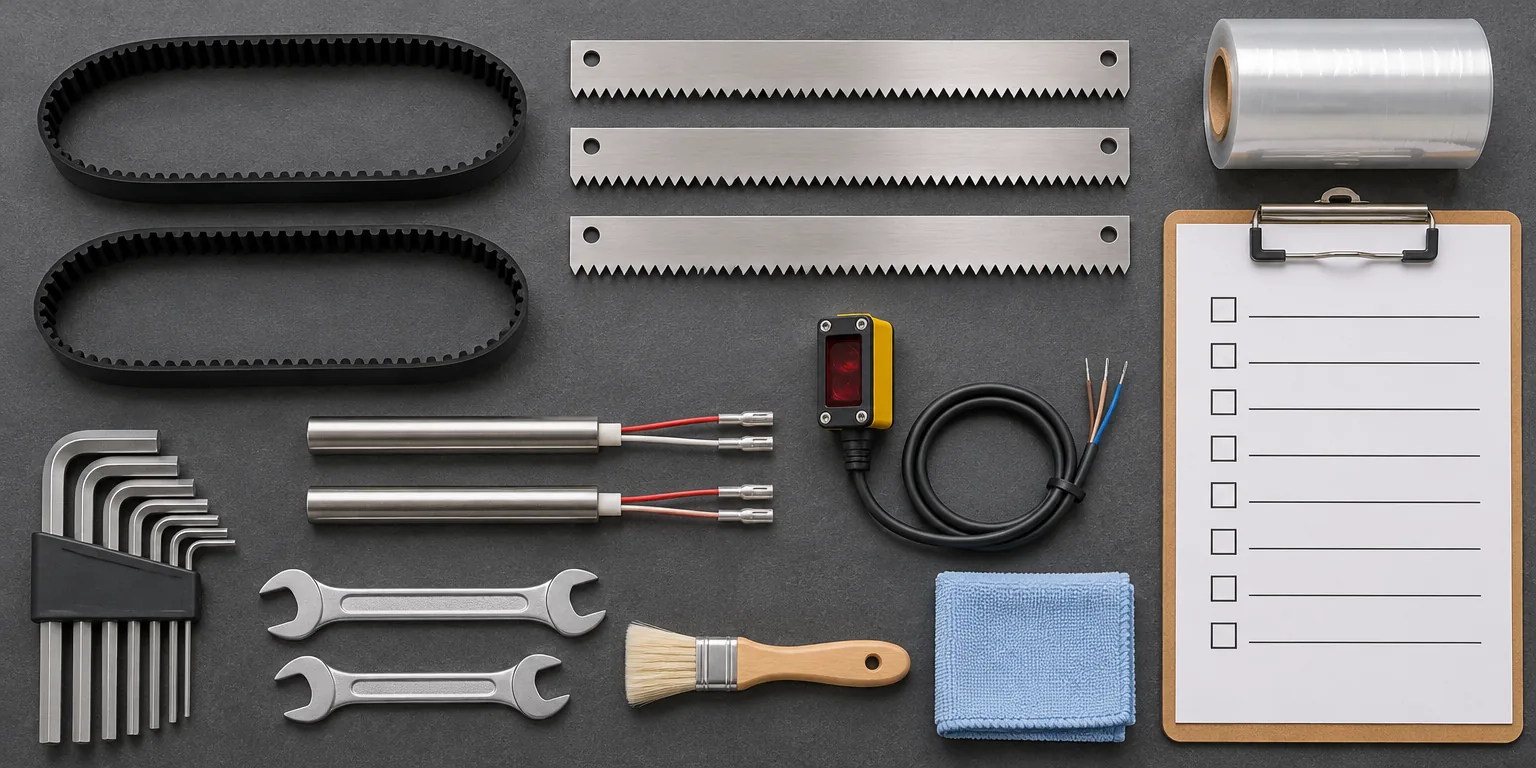
- Regularly: check pull belts for wear and glazing, inspect the forming shoulder and tube for damage, check the knife, check jaw temperatures against the setpoints, check air pressure and filters.
- On schedule: replace wear parts before they fail, lubricate where the manual specifies, and back up machine settings and recipes.
- Always: log every fault, adjustment and part replacement. A fault that keeps returning shows up in the log long before it causes a long stop.
Our preventive maintenance plans are built around each machine, with checklists for what to check, clean, lubricate and replace, and periodic remote checks. Every machine ships with a wear-parts kit that covers normal wear for the first 12 months, and common spare parts are in stock and usually ship within 3 working days.
When to Call for Support
Call when a fault keeps returning, when an alarm points inside the electrical cabinet, or when you cannot find what changed. Send:
- machine model and serial number, or project reference
- what happened, and what changed before it
- alarm screenshot or code
- photos or a short video of the fault
- product and package
- PLC, HMI or software version, where relevant
For our machines, technical support is free and remote, by WhatsApp, video call, video meeting or remote debugging, and we reply within 1 working day. Every machine comes with a remote connection module unless you ask us to leave it out to keep your data private; without it, we work through remote desktop on a computer you connect to the machine.
Questions to Ask Any Supplier
- How do you support the machine remotely, and how fast do you reply?
- Which wear parts ship with the machine, and for how long do they cover normal wear?
- Which spare parts do you keep in stock, and how fast do they ship?
- Does the HMI keep an alarm history I can export or photograph?
- What maintenance plan and checklists come with the machine?
FAQ
Why does my VFFS make bags of different lengths?
Usually the film is not pulled the same distance each cycle, or the print mark is not read reliably. Check the photo eye, the pull belts and the film. A new film batch is a common cause.
Why are my VFFS bags leaking at the seal?
The most common causes are jaw temperature, pressure or dwell that do not suit the film, product or dust trapped in the seal, and dirty or damaged jaws. Check what changed first: the film, the product or the speed.
How often should a VFFS machine be maintained?
Clean the sealing area and photo eye every shift, and schedule checks and wear-part replacement. The intervals depend on your product, shifts and environment, so set them for your machine.
Can VFFS faults be fixed remotely?
Many can. With alarm codes, photos, video and a remote connection to the machine, settings and software faults can often be fixed without a site visit. Worn or damaged parts still have to be replaced on the machine.
Plan for Fewer Stops Before You Buy
Most faults are easier to prevent than to fix. Send your product and film, and we test them on the machine before the configuration is fixed, so the settings, forming set and film are matched from day one.
Request a Packaging Test